Classification variability more than halved
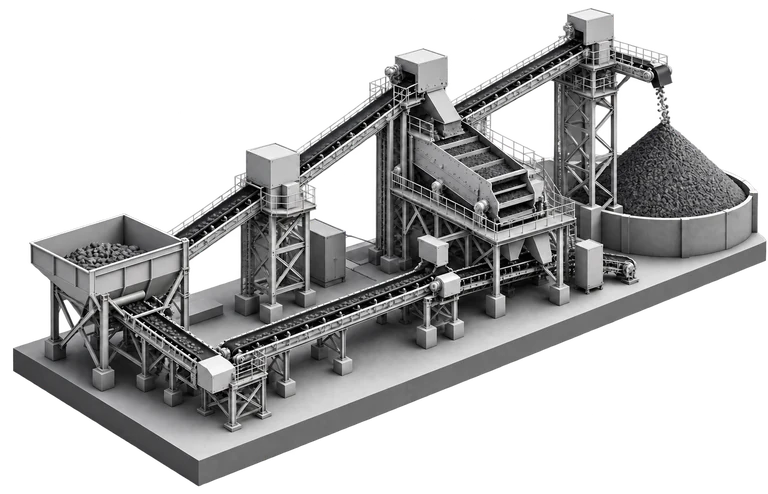
An iron ore concentrator. Hydrocyclone classification, closed loop.
At a glance
| Commodity family | Iron ore |
|---|---|
| Circuit | Hydrocyclone classification |
| Control mode | Closed loop, model-predictive, upper level |
| Assessment | A three-week test period |
| Comparison method | Against the ten most comparable historical periods, matched for product characteristics, sizing, feed chemistry and ore source |
The plant and the problem
Cyclone performance here depended at once on feed rate and density, operating pressure, the level in the feed hopper, pump speed and how many cyclones were open. Controlling pressure alone was not enough: density and load could shift while pressure held steady, and the size at which the cyclones actually separated moved anyway.
The consequence was not confined to classification. Uneven separation made the load arriving at the tailings thickener less predictable. When that vessel approached its limits, operators and the base layer protected it by cutting plant feed. That was the right call each time, and it cost throughput every time. So the classification controller had to absorb short disturbances and hand the next stage a steadier feed.
What was controlled
| Manipulated | Dilution water valve position, feed pump speed setpoint, and the number of cyclones in service as a discrete move |
|---|---|
| Controlled | Feed density and flow, operating pressure, hopper level and pump load, with the separation size cut as the measure of classification quality |
| Constraints | Operating and critical limits on pressure and level, pump power, permitted ranges and rates of change, and minimum and maximum cyclones in service |
| Disturbances | Changes in feed rate and material properties, and which line configuration is actually running |
Continuous and discrete moves were computed together. As load rose the controller could raise pump speed and, if that was not enough, bring another cyclone into service; as load fell it worked back the other way. Only one cyclone could be changed per step. After each move it took fresh measurements and recomputed over a rolling horizon.
The governing idea was that pressure is a means, not an end. It still had a setpoint, but with soft bands around it, so the controller could let it move within its permitted range whenever that stabilised density and the size cut and reduced the swing in load going downstream.
Results
| Metric | Baseline | With closed-loop control | Change |
|---|---|---|---|
| Separation size cut, standard deviation, µm | 6.27 to 6.73 | 2.57 to 3.03 | 2.2 to 2.4 times less |
| Feed density, standard deviation | 0.026 to 0.027 SG | 0.010 to 0.011 SG | about 2.6 times less |
| Controller availability | — | 98% | — |
| Utilisation during the test | — | 90% | — |
No deterioration was observed in product yield or quality, in hopper levels, or in the stability of the receiving vessels, and no operating limit was breached.
What the plant gained
Across the test period the plant ran at a mean feed rate 1.6 to 1.8% higher than in the ten most comparable historical periods, matched for product characteristics, sizing, feed chemistry and ore source. No loss of yield or product quality was observed, and no operating limit was breached.
Where the credit belongs. That gain is the combined effect of the classification and thickener controllers working together. The test material does not separate the contribution of either one, and neither case claims it alone. The figures specific to each controller are the ones in its own results table.
How it was measured
The assessment covers a three-week test period. Comparison is against the ten most comparable historical periods, selected for similar product characteristics, sizing, feed chemistry and ore source, which is a stronger match than a single adjacent baseline would give.
These results describe a defined test period and are not a guarantee of sustained effect. What a longer run would show at this plant, or any result at another, is a separate question.
What this means for your plant
The lesson is not that pressure control was improved. It is that classification was treated as the thing to stabilise, with pressure spent as a resource to do it, and the benefit landed one stage downstream. If your plant reduces feed to protect a vessel that classification is loading unevenly, the constraint you can see may not be the one worth controlling.
See it on your own plant
A desktop review of historian exports. No site visit.