Removing a tailings thickener bottleneck
An iron ore concentrator. Tailings thickening, closed loop.
At a glance
| Commodity family | Iron ore |
|---|---|
| Circuit | Tailings thickening |
| Control mode | Closed loop, model-predictive, upper level |
| Assessment | A three-week test period |
| Comparison method | Against matched historical periods |
The plant and the problem
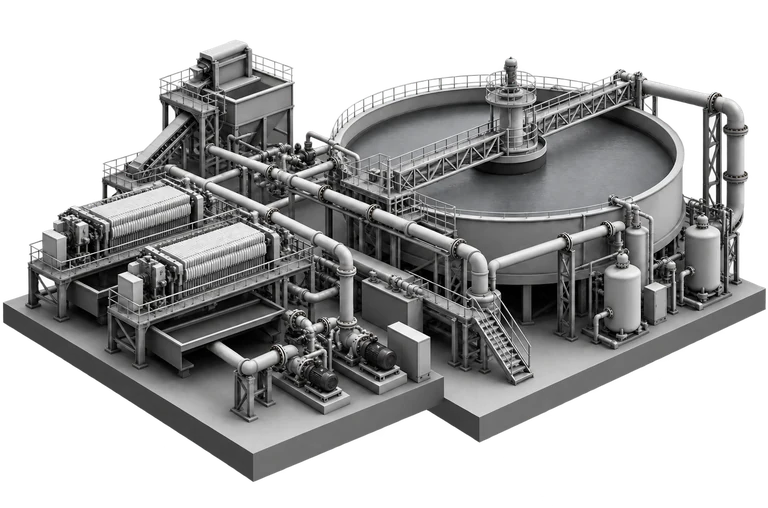
The tailings thickener limited what the plant could process. As solids throughput rose, the bed level rose with it and the rake drive became more likely to hit high torque. When that happened, operators and the base layer protected the vessel by cutting plant feed: technically correct, and a direct loss of production each time.
The existing scheme mainly held the difference between the settled and compacted bed levels by trimming flocculant. If both levels rose together, their difference could stay near setpoint while material quietly accumulated, and the controller would not necessarily notice. The vessel was also affected by the density and pressure arriving from the classification lines, by total plant feed, and by which tailings lines were running. What was needed was coordinated control of a slow process whose priorities change: settle normally, but as the torque limit approaches, get the vessel back into safe territory before anyone has to cut feed.
What was controlled
| Manipulated | Specific flocculant dosage setpoint, bounded in both range and rate of change |
|---|---|
| Controlled | Bed level and pressure, interface position, the difference between settled and compacted bed levels, rake drive torque and overall tailings density |
| Constraints and priorities | Operating and critical torque limits, permitted bed level and pressure range, dosage limits. Approaching a critical state, preserving margin outranks ordinary stabilisation |
| Disturbances | Density and pressure from the classification lines in service, total plant feed, and flow through the running tailings lines |
Underflow withdrawal, which sets bed inventory and bed pressure, remained under the plant's existing control. The new controller sat above it and acted through flocculant dosage alone.
The controller forecast several variables over a horizon matched to the slow dynamics of a thickener, then chose an allowable change in dosage. It did not chase one number at the expense of others: it held the level difference while also preventing excessive accumulation, high torque and bed excursions, using soft constraints to find a safe compromise when those goals conflicted. Nearing the critical torque limit, priorities shifted in advance, before a sharp feed cut became necessary.
Thickener control was coordinated with the classification controller. It accounted for which lines were running and the load they were creating; steadier classification meant smaller swings in incoming load, so the vessel approached its limits less often.
Results
| Metric | Baseline | With closed-loop control | Change |
|---|---|---|---|
| Time in high rake-torque events | — | — | about 1.1 hours per day less |
| Mean bed level | 19.91% | 16.75% | −3.15 points |
| Interface level | 22.19% | 19.76% | −2.42 points |
| Flocculant consumption | 55.87 g/t | 53.22 g/t | −2.65 g/t |
| Mean bed pressure | 85.21 kPa | 85.61 kPa | Essentially unchanged |
Bed pressure barely moved and the spread of the level difference was unchanged, which matters: the result was not obtained by running the vessel harder or at higher pressure. The thickener spent less of its time in the states that forced a feed cut, and did so on less flocculant. The gain comes from avoiding over-flocculation: excess flocculant raises the yield stress of the bed and with it rake torque, so trimming the dose cut time at high torque without giving up settling.
What the plant gained
Across the test period the plant ran at a mean feed rate 1.6 to 1.8% higher than in the ten most comparable historical periods, matched for product characteristics, sizing, feed chemistry and ore source. No loss of yield or product quality was observed, and no operating limit was breached.
Where the credit belongs. That gain is the combined effect of the classification and thickener controllers working together. The test material does not separate the contribution of either one, and neither case claims it alone. The figures specific to each controller are the ones in its own results table.
How it was measured
Time at reduced feed was measured at 1.19 hours per day less than in matched historical periods, with an estimated range of 0.94 to 1.43 hours. The thickener variables are compared against the same matched periods.
Directly demonstrated for this vessel are the reduction in high-torque events and the changes in its own operating variables. The plant-level feed gain is joint, as above.
These results describe a defined test period and are not a guarantee of sustained effect. What a longer run would show at this plant, or any result at another, is a separate question.
What this means for your plant
A thickener that occasionally forces a feed cut is rarely counted as a bottleneck, because it is not running out of capacity; it is running out of margin. The hours it costs are visible in your historian, and they are usually the cheapest throughput on the plant to recover.
See it on your own plant
A desktop review of historian exports. No site visit.